PEILIBRUSHLESS

Manufacturing

From stator winding to a finished 605 pump — on one line.

Jiangmen winds the segmented stator, forms the ring and overmolds it in BMC, then mates the motor to the 605 diaphragm head. Incoming inspection, in-process checks and nine outgoing benches — leak, flow, pressure, load and noise — qualify every unit on the same campus that already supplies first-line purification OEMs.

2015

Founded

10,000+

m² campus

200k

units / month

50+

patents

150+

people

9

test benches

The factories

Design, noise work and type testing stay in Shunde. Volume metal, plastic and motor processes sit in Jiangmen, in the western Greater Bay Area, with the rotor company on the same industrial chain.

Shunde, Foshan

R&D headquarters

Building 1, Huazhi Science Park, 28 Sanle East Road, Beijiao, Shunde

PEILI’s technology centre sits in Beijiao, Shunde — China’s home-appliance cluster. The building holds product development, an anechoic chamber for pump and complete-machine noise work, and the nine performance benches that qualify every new drawing before it reaches Jiangmen.

Xinhui, Jiangmen

Manufacturing base

Shenjiang Industrial Park, Xinhui District, Jiangmen, Guangdong–Hong Kong–Macao Greater Bay Area west wing

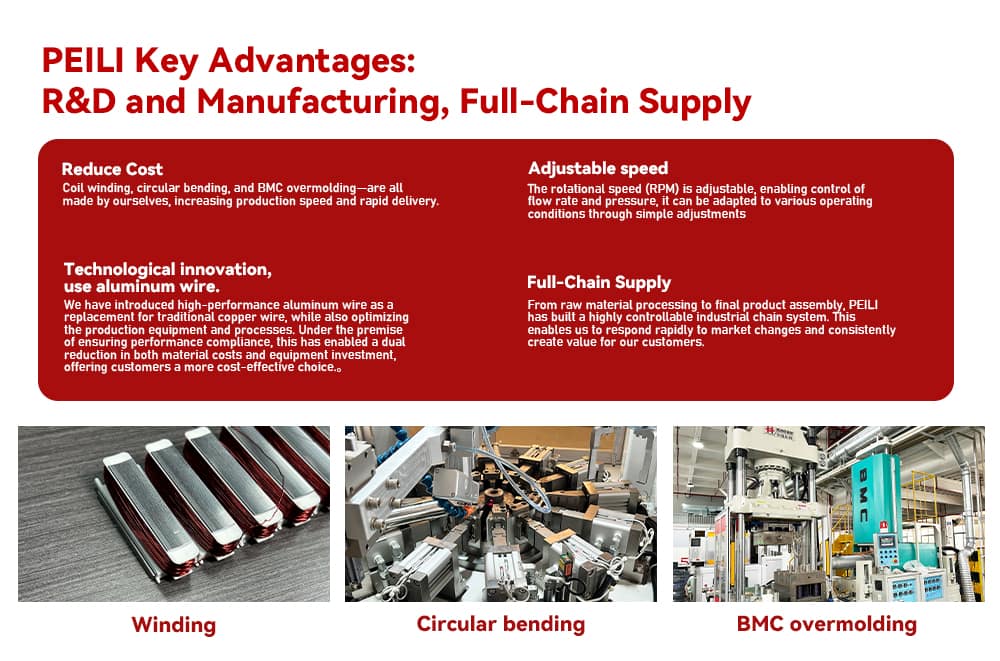
The plant is a self-built base in Shenjiang Industrial Park. Three intelligent final-assembly lines run under servo control, with a rated 200,000 units a month. Coil winding, ring forming and BMC overmolding for the brushless stator happen here — the motor is not a bought-in can.

Jiangmen Peili Chiyang Motor

Rotor manufacture

Jiangmen, Guangdong

The rotor — the part that decides magnetic torque and hydraulic delivery — is made by Jiangmen Peili Chiyang Motor, a PEILI company. Vertical supply of this core keeps lead time and magnetic consistency inside the group.
What the Jiangmen line actually makes

Tooling and injection sit upstream of the brushless stator. The cell then winds, ring-forms and BMC-overmolds the motor, and assembles it to the 605 diaphragm head as a complete pump before the nine outgoing benches.

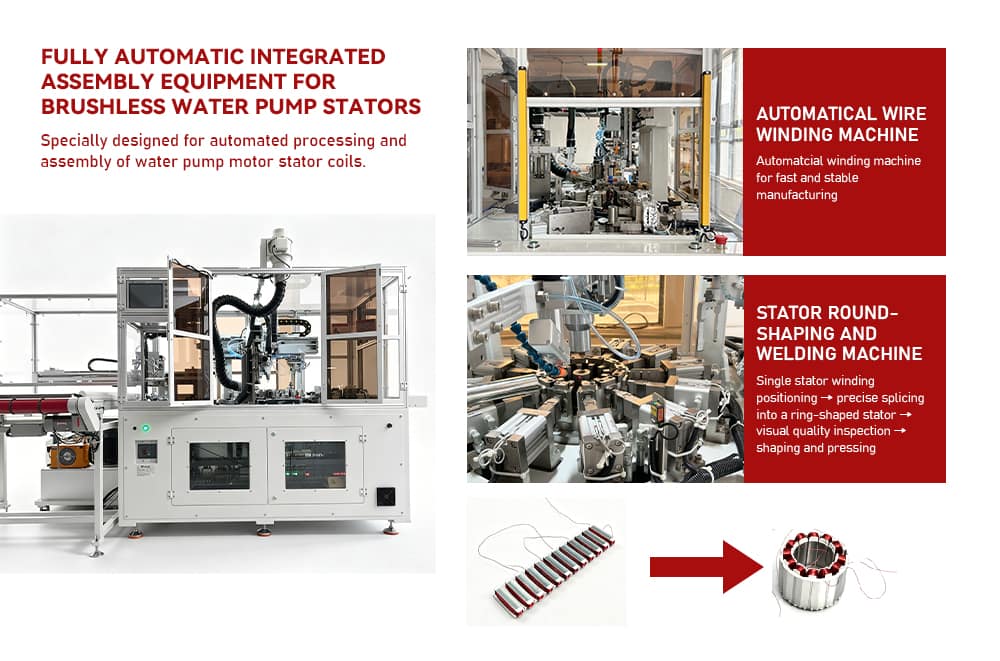
Winding

Winding

Segmented stator coils are wound in-house on automatic machines to a controlled turn count — consistent resistance, inductance and thermal margin from lot to lot.

Circular forming

Circular forming

Individual segments are indexed, spliced into a closed ring, inspected, then pressed into a stator core ready for encapsulation.

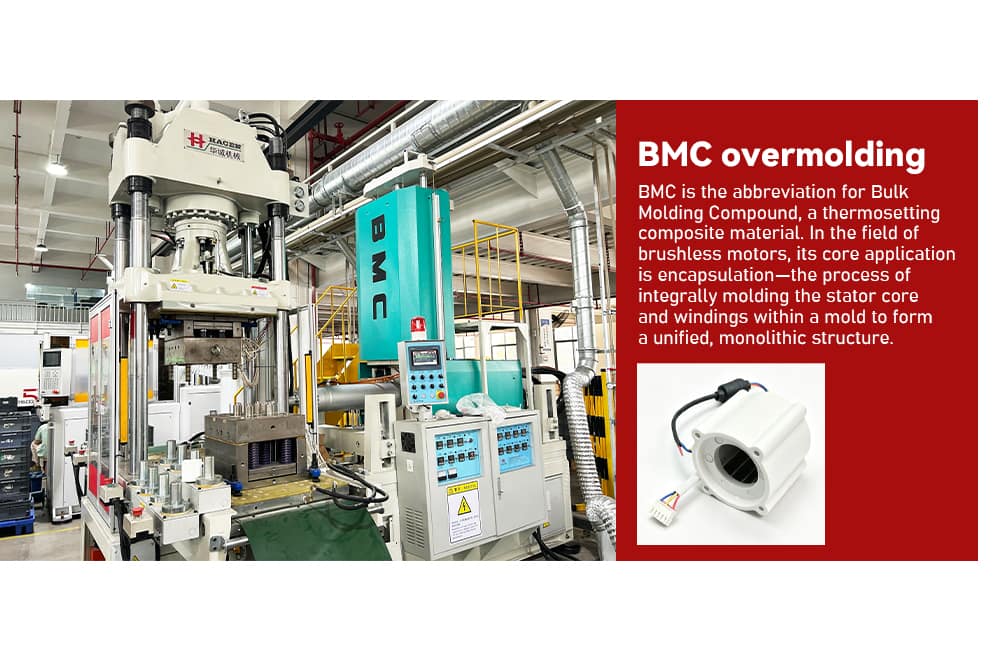
BMC overmolding

BMC overmolding

Bulk Molding Compound encapsulates the ring stator in a single thermoset shot — dielectric strength, rigidity, heat path and sealed cosmetics in one cycle.

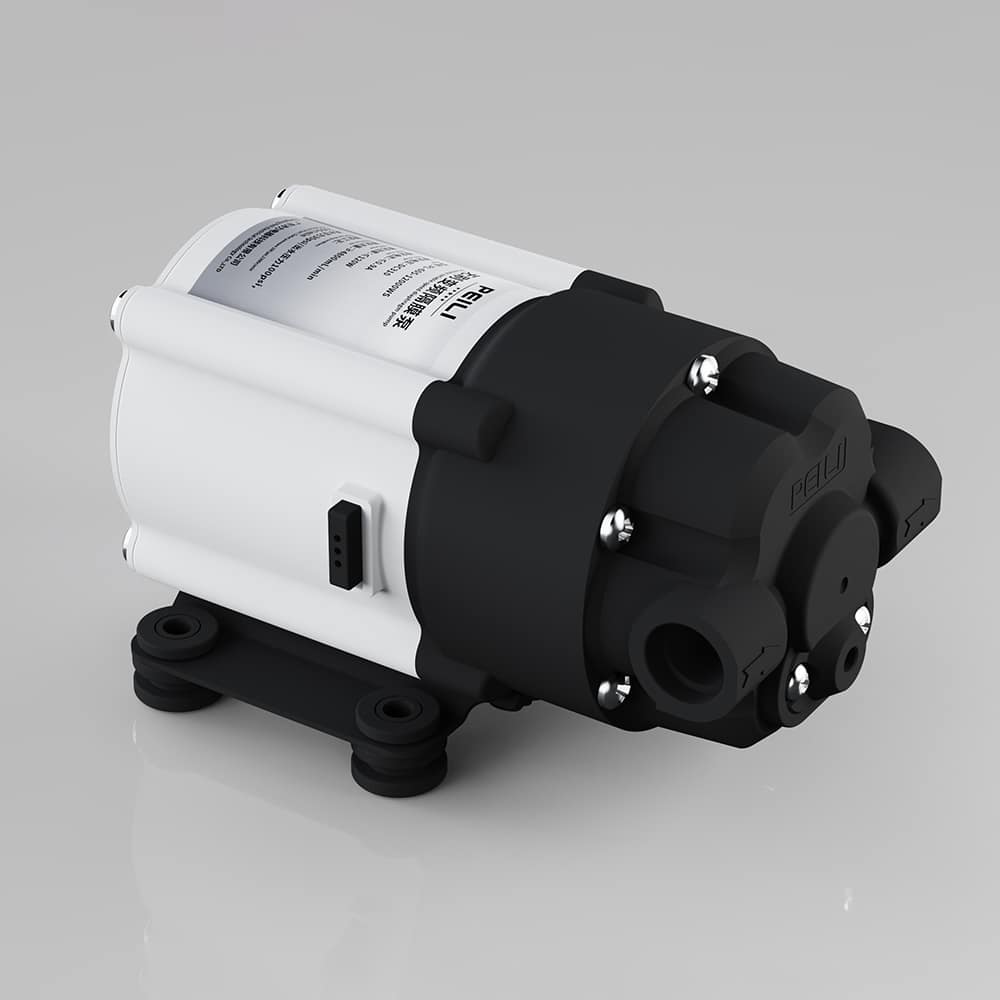
Pump assembly

Pump assembly

The finished motor is mated to the 605 diaphragm head, valves and ports. The complete pump is leak-checked and run to its rated point before packing.

Nine benches before it ships

Burst and water-hammer work that already sits behind PEILI’s brushed 605 line applies to the same wet-end family. Electrical, sealing and hydraulic data are stored per unit on the automated water test stand.

Air tightnessMechanical propertiesFlame retardanceFlow performanceNoisePressureLoadHot / coldMaterial reliability
ISO 9001:2015CERoHSREACHFDA-grade wetted partsCQCNational High-tech EnterpriseSpecialized & Sophisticated SME
WhatsAppEmail